
Conveyor Engineering
ABM Equipment provides comprehensive conveyor engineering services for food, pharma, chemical, and packaged goods applications. Our experienced process engineers ensure you’re using the optimal conveyance method, that the equipment is built with the optimal materials and features, and that the final system operates as a cohesive unit. When needed, our mechanical engineers then custom-design conveyor models for your application and our fabrication department integrates and supports your system going forward.

For ALL conveyors including tubular, vibratory, screw, and pneumatic.
From initial design to installation and maintenance, we ensure that your conveyors and systems are optimized for efficiency and reliability.
Our conveyor engineering services begin with a thorough analysis of your specific needs and operational requirements. We take into consideration factors such as material and product characteristics, flow rates, and space constraints to design a conveyor system that maximizes productivity and minimizes downtime.
By choosing our conveyor engineering services, you can benefit from our in-depth knowledge of conveyor systems and our commitment to delivering high-quality solutions. We utilize the most recent technology and industry best practices to ensure that your conveyor system moves your product efficiently and safely.
We have a broad range of experience in most types of material handling and logistics applications and understand that equipment is ultimately useless if it’s not supported. We service what we sell by policy, provide 24/7/365 support for customers, and offer preventative maintenance agreements to ensure maintenance schedules aren’t neglected.
Reasons Conveyors and Conveyance Systems Need Customization
Unique Operational Needs
Each application and space has its own unique operational needs whether it’s space constraints, environmental threats, or integrating with existing equipment, and it can be very difficult to find out-of-the-box models with the right mix of features and tolerances. By tailoring the system to your needs, we can optimize efficiency and your bottom line. We can customize location of service panel, upgrade the washdown rating, change how the belts or screws are removed, add dust control integration, change the mounting method of drives and accessory tools, or virtually anything else that needs to be done.
Varying Material Characteristics
Materials being transported can vary greatly in size, shape, and characteristics. Having a custom system allows you to harness or accommodate these traits to prevent product damage and optimize flow. A few days of engineering time can save hundreds of days on the floor.
Process Integration
Conveyor systems need to seamlessly integrate with other processes and equipment in your facility. By customizing your conveyors from the beginning, we can ensure smooth integration, efficient material transfer, and minimized bottlenecks.
Cost Savings
Custom conveyor systems can be more cost-effective up-front by ensuring that you only invest in the features and capabilities that essential to your operation. They can also save money in the long-run by reducing wear on the conveyors and product.
Why Choose Us
Experience
With over 40 years of experience across a number of industries—and most likely with products like yours—we bring an understanding of your materials and how they will behave in different circumstances. This allows us to reach better solutions without reinventing the wheel or bringing in third parties.
Quality and Reliability
ABM Equipment has long been committed to systems that make sense in the long-run. From the selection of materials to the utilization of technology, we prioritize quality and reliability in every aspect of our work. Our systems can be built to endure harsh environments over long periods of time.
Comprehensive Services
Our conveyor engineering services cover the entire project lifecycle, from design to maintenance. Our end-to-end approach offers a headache-free experience for your operations and project managers. Our team is always available to provide support throughout the project.
Fill out the form below or give us a call to find out how we can add value to your project!

Screw Conveyors
Screw conveyors are one of the oldest conveying methods known to man and still the ideal method for many applications. Though screw conveyors and augers are technically synonymous (any conveyance method driven by rotating threads) the processing industry typically reserves the term “screw conveyor” for larger executions, and augers for enclosed, tubular conveyors. For precise metering using screws, see screw feeders.

Magnetic Conveyors
Home » Ingredient Handling Equipment » Conveyors Magnetic conveyors use magnetic…
Vibratory Conveyors
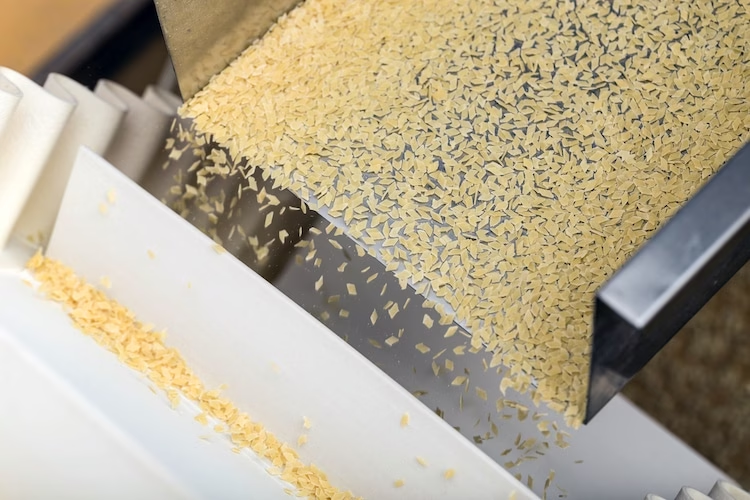
Vibratory conveyors vibrate a sloped metal plate to make loose solids flow. We use them for many products that need gentle, short-distance conveyance, most commonly pharmaceuticals and ingredients. We integrate the flat, open designs that most people are used to seeing as well as tubular 3A models.
Spiral Conveyors
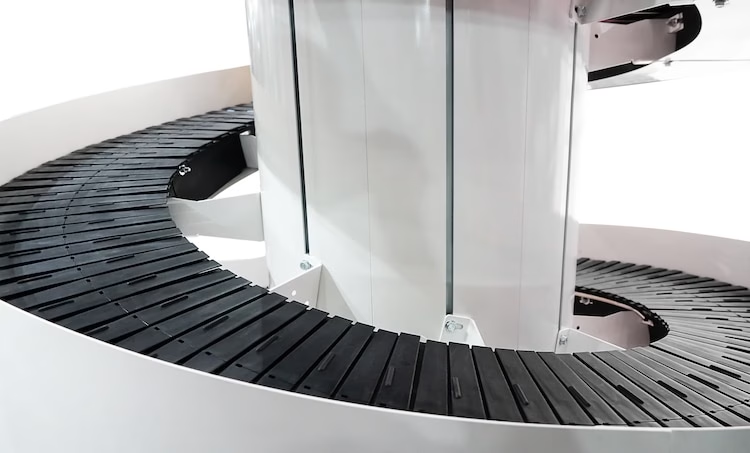
ABM supplies spiral conveyors to move units of product vertically where floor space is limited, space is needed for accumulation, or the product needs more dwell time on the best for cooling. We provides spiral conveyors from a number of different OEMs depending on the best combination of quality, cost, and features for your application. From selection and drawings to customization and integration, ABM handles your project from conception to maintenance.
Tubular Drag Conveying Systems
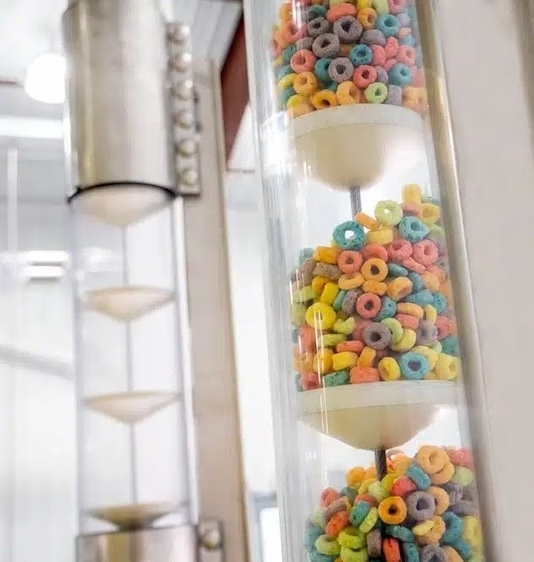
ABM supplies tubular drag conveyors for most non-abraisive, free-flowing products including powders, pellets, and granules. Capacities can vary depending on the configuration and product, but as a reference, tubular drag conveyors reach capacity with milled grain at 2,000 ft. through 24 elbows and conveying at a rate of about 300 pounds per hour.

Tube Belt & U-Belt Conveyors
Home » Ingredient Handling Equipment » Conveyors We use tube and u-belt conveyors most…

Bucket Elevators
ABM uses bucket elevators are to lift bulk dry ingredients within a small footprint. They consist of a series of buckets attached to a belt or chain, which runs over a pulley or sprocket at the top and bottom of the unit. The buckets scoop up material at the bottom and then lift it to a higher point, where the ingredient is discharged.

Chain Conveyors
Chain conveyors, not to be confused with chain-driven belt conveyors, or tubular drag, use gear-driven chains to move materials along a conveyor path. ABM provides different configurations to move large, heavy objects such as boxes and pallets, or varous kinds of loose material with specialized paddles.