
Vibratory Conveyors
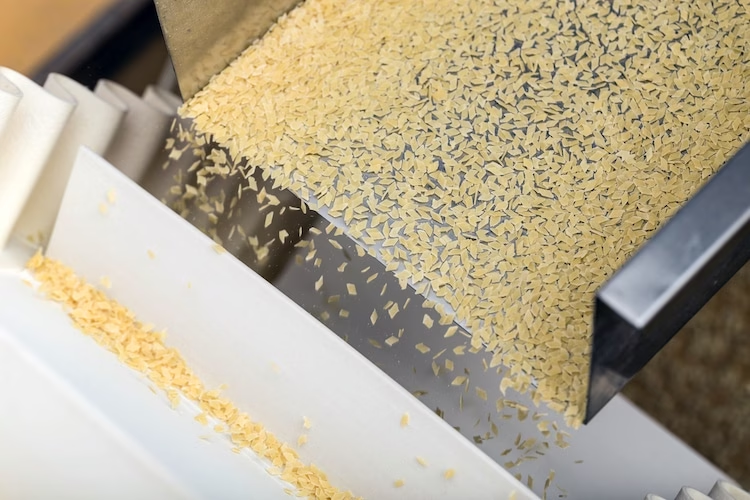
Vibratory conveyors vibrate a sloped metal plate to make loose solids flow. We use them for many products that need gentle, short-distance conveyance, most commonly pharmaceuticals and ingredients. We integrate the flat, open designs that most people are used to seeing as well as tubular 3A models. (Looking for vibratory feeders? Go Here.)
Types
- Electromagnetic Vibratory Conveyors: We use electromagnetic vibratory conveyors when handling fine powders—like in pharma—where large motors are overkill and you want finer control over the product flow. These conveyors simply use an electromagnetic drive to create a linear vibratory motion that moves the material forward instead of motors, and will have little effect on larger ingredients, like grains.
- Mechanical Vibratory Conveyors: Mechanical vibratory conveyors are what most people think of when they think of these classes, and use (a) motor(s) to create vibrations that cause bulk solids to flow like a slurry. We use them for dry, non-sticky ingredients that need to be moved precisely and gently.
- Spiral Vibratory Conveyors: We use spiral vibratory elevators for delicate product that needs to change elevation without damage. But because gravity is a precious commodity on the processing floor, conveying downward is rarely needed. Using vibration to make bulk solids flow downward makes sense to everyone, but they can also be used to move product upward. Here's how: when configuring a vibratory screener, you tune the vibration of each motor either in harmony with or conflict against the other, and this changes the way the product flows. With a spiral vibratory elevator, you tune them to move the product against the uphill slope of the conveyor, which moves product upward.
- Tubular Vibratory Conveyors: We typically use tubular vibratory conveyors in sanitary—usually 3A dairy—applications where the conveyor's contents need to be protected from the environment. These conveyors no different from normal vibratory except that they're round, enclosed, and usually sanitary.
- Vibratory Screen Conveyors: Vibratory screens are a type of vibratory conveyor that are designed to screen materials based on their size or shape. These conveyors use a series of screens or mesh panels that vibrate to separate the material into different sizes—or just screen off smaller particles—while the product is moving. Looking to screen but not move? See vibratory screeners here.
Benefits And Drawbacks
Many benefits and drawbacks of vibratory conveyors will depend on the product. For example, strong but brittle products will find vibratory conveyors much more gentle than others, while heavy and friable materials will find them unacceptably rough. Similarly, there is a conveyor slope for each product after which vibratory will become more efficient than belted. If there's any grey area in your application, give us a call or fill out the form below to know for sure what will be best.
Benefits
- Great for Metering: Vibratory conveyors can be controlled very finely, giving us control over how quickly or slowly the product moves—if turning the motor down or up doesn't give us the control we want, we can change the offset of the motor(s) to make adjustments less or more coarse. Additionally, you can slow it down without stopping other equipment. When it's slowed down and product piles at the entrance, the pile will distribute itself across the conveyor to a degree—instead of creating a pile that stays there and enters the process all at once, like with a belt conveyor.
- Easy to Maintain: Vibratory conveyors usually have an open design, making them easy to tinker with if something needs changed. But this is rarely needed because of the simplicity of the design and absence of wear parts. A good motor will last decades and it takes quite a bit longer than that for cornflakes to wear through stainless steel.
- Great Range: Not only does vibration work well for many different products, but the speed can be changed over wide ranges. With conveyor slope, vibration intensity, and motor orientation all at our disposal, one conveyor can move product very slowly or very quickly without damaging the conveyor or making it wear more quickly.
Drawbacks:
- Noise: Vibratory conveyors can be relatively noisy, especially if they are not properly maintained. This isn't a concern with smaller units, however.
- Not Good For All Applications: Obviously slurries already flow without vibration, and sticky products won't flow with or without vibration—so we can't use them for everything.
Why ABM?
ABM is more than just a connection to OEMs. With over 20 years of experience in the industry, we have built a reputation for providing high-quality, reliable, and effective conveying solutions to a wide range of industries.
With a team of experienced engineers and technicians, we provide customized solutions to meet the specific needs of our customers. We work closely with you to understand your requirements and recommend the most suitable conveyance configuration for your application.
We offer ongoing service and maintenance for our packaging systems to ensure they continue to operate at optimal performance. Our technicians are knowledgeable and experienced, and are available to provide on-site maintenance, repair and support services.
Whether you are looking for a single piece or a cohesive system, ABM Equipment can help scale and automate your process. Contact us below to learn more about our services and how we can help you achieve your production goals.