
Spiral Conveyors
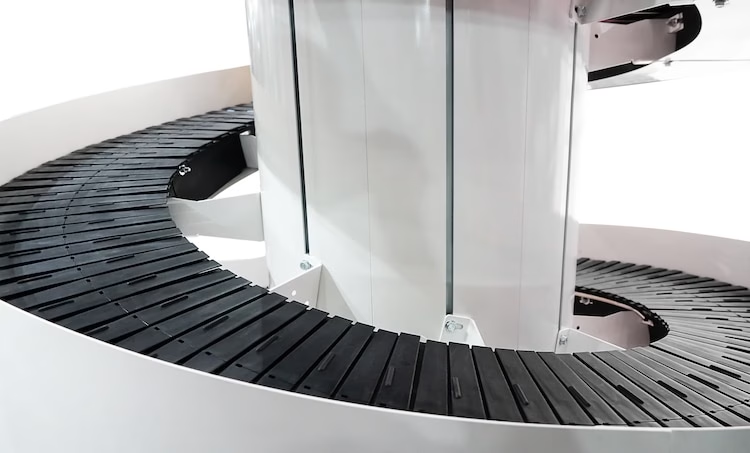
ABM supplies spiral conveyors to move units of product vertically where floor space is limited, space is needed for accumulation, or the product needs more dwell time on the best for cooling. We provides spiral conveyors from a number of different OEMs depending on the best combination of quality, cost, and features for your application. From selection and drawings to customization and integration, ABM handles your project from conception to maintenance.
Materials
Carbon Steel
Carbon steel is a bit cheaper than stainless, so it's practical when you don't need to it to be food grade or washdown. Because most spiral conveyors are either used for non-food or food after packaging, powder-coated carbon is the material you'll see used most commonly.
Stainless Steel
Stainless steel is the more expensive but food-grade option, and most OEMs offer it. Hygienic spiral conveyors with sanitary designs are less common as they are more difficult to make, but there are still plenty of options.
Configurations
Spiral conveyors can be configured to meet any demand placed by your application: pitch, line height, belt return method, belt type, etc. If no spiral conveyor is optimal for you out-of-the box, ABM can customize the design for the closest OEM to manufacture.
Single Lane
Single lane spiral conveyors are the simplest and most common configuration. They consist of a single spiral that transports materials vertically between two levels, while the return belt makes a direct, vertical return to the infeed.
Dual Lane
Dual lane spiral conveyors are used when more than one product needs to be transported vertically. They consist of two spirals that are stacked on top of each other and run in opposite directions. Dual lane conveyors are ideal for applications where materials need to be separated or sorted.
Vibratory
Spiral conveyors are available in vibratory configurations, which will take up less footprint and use less energy than their belted counterparts.
Benefits
Space: Spiral conveyors can move product vertically without taking up a lot of space.
Dwell Time: When product needs room to accumulate, warm up, or cool off, spiral conveyors give your product time to do that.
Drawbacks
Cost: Spiral conveyors are more expensive than straight.
Maintenance: Though they don't require more maintenance than other methods with comparable features, it will become less convenient to reach the areas you need to maintain.
Why ABM?
ABM is more than just a connection to OEMs. With over 20 years of experience in the industry, we have built a reputation for providing high-quality, reliable, and effective conveying solutions to a wide range of industries.
With a team of experienced engineers and technicians, we provide customized solutions to meet the specific needs of our customers. We work closely with you to understand your requirements and recommend the most suitable conveyance configuration for your application.
We offer ongoing service and maintenance for our packaging systems to ensure they continue to operate at optimal performance. Our technicians are knowledgeable and experienced, and are available to provide on-site maintenance, repair and support services.
Whether you are looking for a single piece or a cohesive system, ABM Equipment can help scale and automate your process. Contact us below to learn more about our services and how we can help you achieve your production goals.