From stick packs and sachets to bottles, pouches, cartons, trays, and multipacks, ABM delivers the level of quality and automation that fits your process and budget.
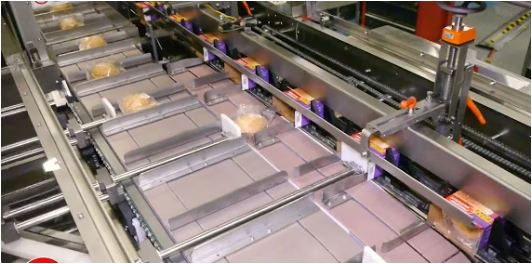

ABM specializes in powdered dairy applications from proteins to mixes, agglomeration to deagglomeration. From individual equipment to complete systems, ABM delivers storage, intake, weighing, batching, milling, sifting, packaging, dust collection, and inspection systems. Browse common equipment below or get in touch to find out how we can add value to your project.
From stick packs and sachets to bottles, pouches, cartons, trays, and multipacks, ABM delivers the level of quality and automation that fits your process and budget.

ABM integrates all configurations of magnets in lines to protect consumers and equipment from stray metals. We carry all types of magnets from drawer and hump to torpedo and plate.
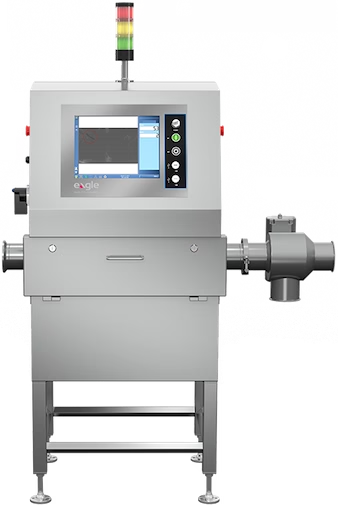
The liquid X-ray model (pipeline from Eagle) is used for all types of liquid products from soups and slurries to ground meat. It employs a flow meter to improve the image consistency—which makes contaminants easier to find—and a diverter valve to reject contaminated segments of product.
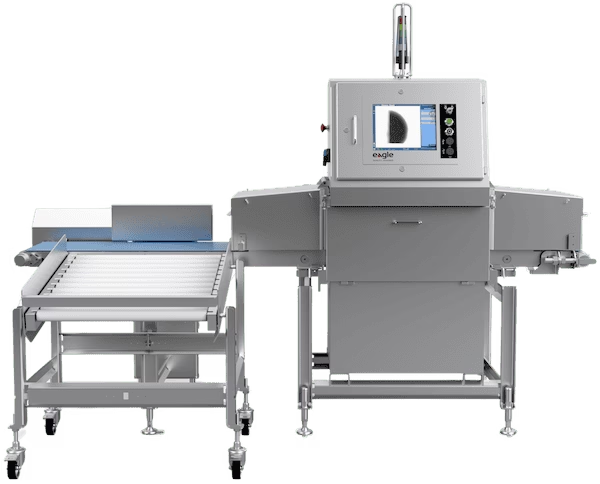
The 3-A hygienic version of the mid-sized X-ray machine for standard packages is the most popular unit for cheese applications. With a 400mm (15.7”) belt width it is a popular option for producers of wrapped and unwrapped cheese. Many features, which are expanded on below, make cleaning easy and improve hygiene.

In an automated process where silos and bulk bag unloaders are feeding closed conveyors (pneumatics or tubular drag), operators need a way to add extra ingredients to the system. Bag dump stations provide a convenient, safe way to do this. ABM Equipment’s bag dump station has a unique mix of features that eliminate waste and reduce man-hours.

Whereas ribbon blenders create opposing streams in a vessel, paddle mixers create a tumbling effect by lifting the mix and letting gravity do the rest. This method is the gentler way of mixing product, though it may be slower per cubic foot of mixer volume. ABM provides and integrates virtually every configuration of paddle mixer with customizations (when necessary) for your product.

Hybrid mixers combine the agitators from ribbon and paddle mixers. This can be useful for products that are too delicate for ribbon mixers but won’t be mixed well enough by paddles, or for mixes which mound. The combination of these two methods has the convenient tendency to keep product from clumping up in the middle of your mixer.

Fluidizing blenders, or fluidizers, are a class of paddle blender meant for mixing finely divided solids with varying densities. When compared to paddle blenders, the paddles are smaller, more angular, set at decreasing distances along the shaft, and spun more quickly.

Ribbon blenders are one of the oldest automated mixing methodologies and use u-shaped troughs with opposing sets of helical agitators—one inner, and one outer. By forming 2 opposing cyclones within the product, they create homogeneous mixes quickly but create some heat and can degrade sensitive products.
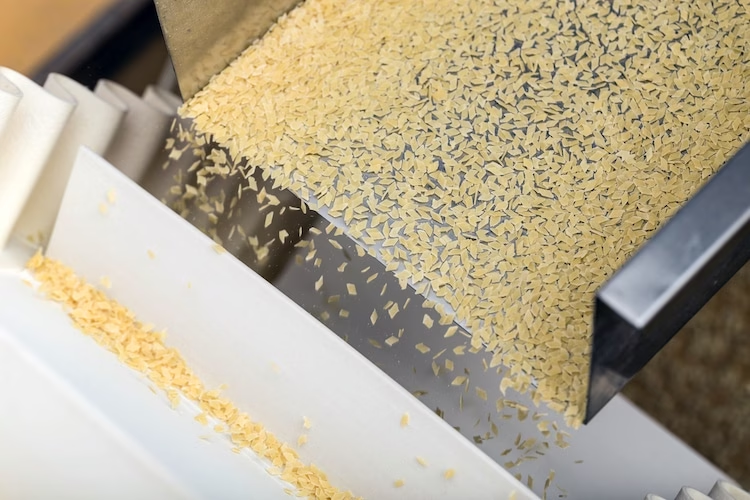
Vibratory conveyors vibrate a sloped metal plate to make loose solids flow. We use them for many products that need gentle, short-distance conveyance, most commonly pharmaceuticals and ingredients. We integrate the flat, open designs that most people are used to seeing as well as tubular 3A models.
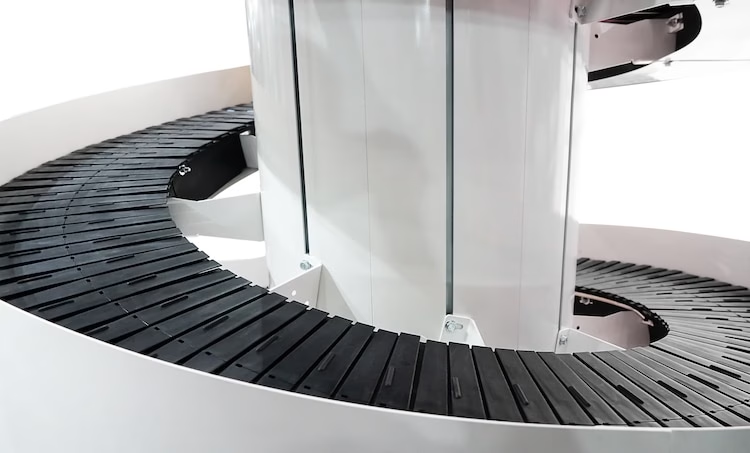
ABM supplies spiral conveyors to move units of product vertically where floor space is limited, space is needed for accumulation, or the product needs more dwell time on the best for cooling. We provides spiral conveyors from a number of different OEMs depending on the best combination of quality, cost, and features for your application. From selection and drawings to customization and integration, ABM handles your project from conception to maintenance.

The vibratory screeners we carry (Russell for hygienic and Kason for all others) are available from 18-100″ diameters with up to 5 decks and any combination of optional configurations to fit any project. These optional configurations include sanitary, gap-free, lift-assist lids, CIP, various solutions for difficult products, ultrasonic, and more.

We provide bulk bag unloaders (BBUs) for food, nutraceutical, pharmaceutical, and chemical manufacturing systems. There are many configurations available on the market, so whether we source or build them will depend on your needs. The benefits of moving to BBUs (assuming your ingredient demand warrants them) are listed below.

ABM fabricates and sources work bins of all types, from totes on wheels to product staging in continuous processes, in all metal materials from carbon and stainless to aluminum. We handle install, integration, and service on all intake and discharge conveyance as well as surrounding equipment.

ABM distributes Kason fluid beds for many applications including agglomeration and drying. Available up to 72″ in diameter, ABM integrates, supports, and modifies fluid bed dryers when necessary.

ABM Equipment provides both powered and gravity roller conveyors for boxes and large packaged goods in manufacturing, warehousing, and distribution applications. We use powered roller conveyors for controlling product spacing, controlling speed of incoming product, and conveying different products independently on the same conveyor.

Baghouses, or bag filters, are a type of dust collection system that uses filter bags to capture and remove dust and other particulate matter from industrial processes. These systems are commonly used in a wide range of industries, including cement, mining, power generation, and metal production, to remove particulate matter from the air.
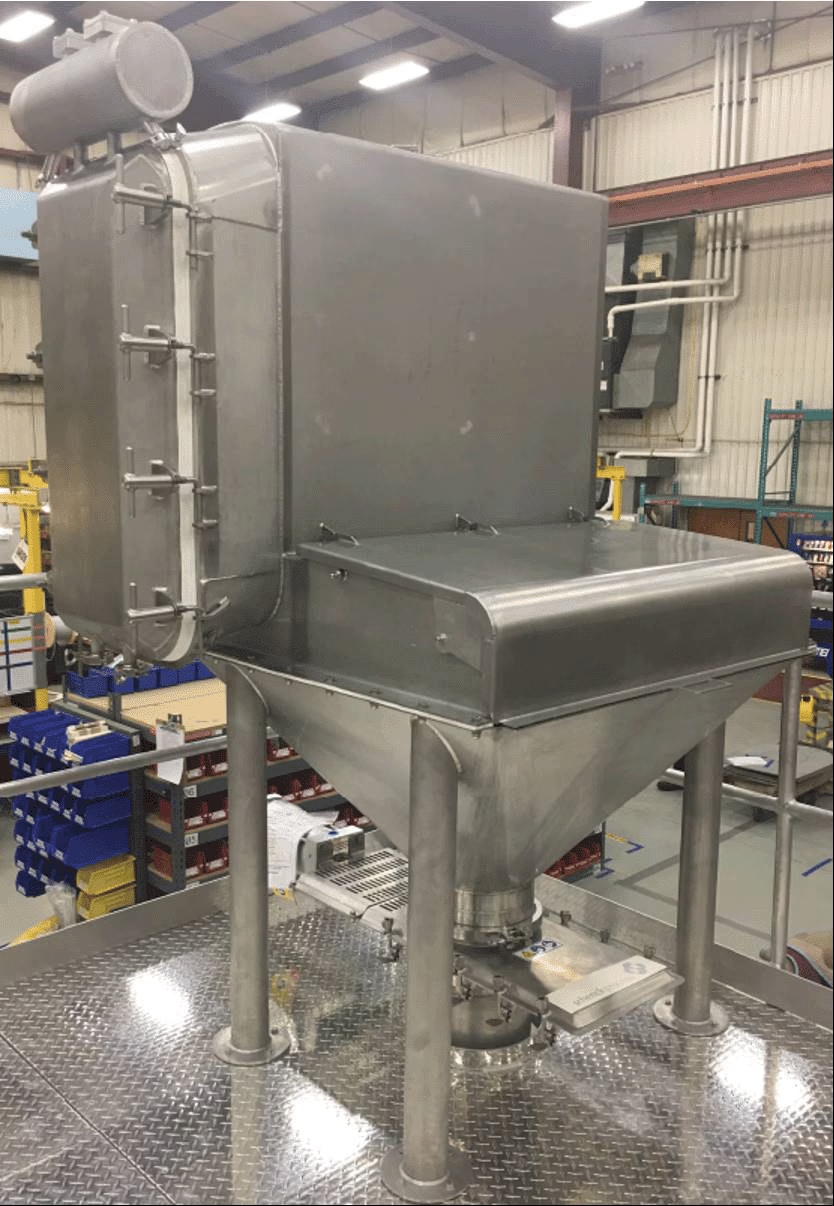
ABM supplies cartridge dust collectors for applications where 1, granular filtration and easy maintenance are priorities over maintenance cost and 2, where space is limited. Filters can be round or rectangular, and made of natural or synthetic materials depending on the application.
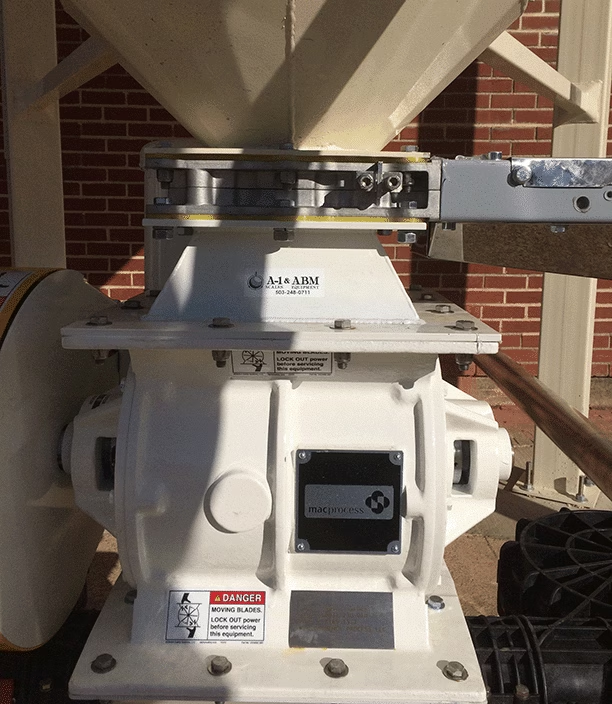
ABM provides rotary valves as flow control devices for the conveyance of powders, granules, and other bulk materials in ingredient handling systems. ABM handles system design, integration of rotary valves and connected equipment, and service for the life of your system.
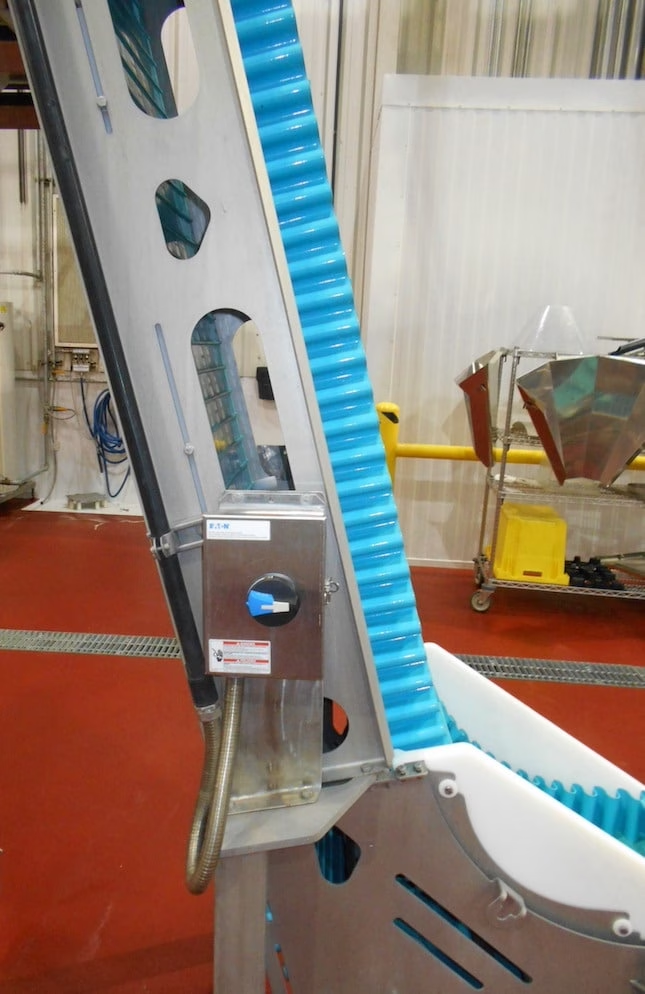
Corrugated belts feature walls which are expandable so they can wrap around pulleys, and are often combined with cleats to form buckets. Although we primarily use corrugated belts food processing plants as pictured here, they are also used in outdoor industrial applications because they can contain product when it’s being jostled about over uneven terrain.

ABM supplies lump breakers to reduce particle size of large lumps or aggregates. Often used in the processing of bulk ingredients such as chemicals, pharmaceuticals, and food products, we integrate them in systems like yours to improve a material’s flow, make it more compactable, or prepare it for milling.

We offer several models in each of the divisions below to accurately dispense product in the needed increments whether grams or hundreds of pounds. Industrial to 3-A Dairy and washdown, we can integrate any feeder with conveyors, other equipment, and software.